Lightweight yet powerful, the large capacity refrigerated centrifuge factory continues to raise the standard for efficiency of operation. High-performance control algorithms provide instant acceleration and smooth deceleration, protecting delicate samples from stress. Dual cooling systems provide thermal stability in even long runs. Modular design provides easy maintenance and upgrading. Remote diagnostics and system optimization connectivity is available in some models. Along with these advancements, the large capacity refrigerated centrifuge factory becomes a bridge between traditional engineering and modern automation and functions as a pillar of accurate, high-rate separation within labs and factories around the world.

large capacity refrigerated centrifuge factory are part and parcel of the functioning of modern laboratories and factories. Applications include cell culture harvesting, purification of enzymes, and waste handling. In oil processing, they facilitate hydrocarbon/water separation. Clinical laboratories depend on large capacity refrigerated centrifuge factory for accurate diagnostic tests, and chemical industries use them to purify chemicals and recover active ingredients. They also hold great importance in educational research, where repetition and accuracy are necessary to experimentation. This wide application reveals the extent to which large capacity refrigerated centrifuge factory continue to drive scientific and industrial advancement globally.
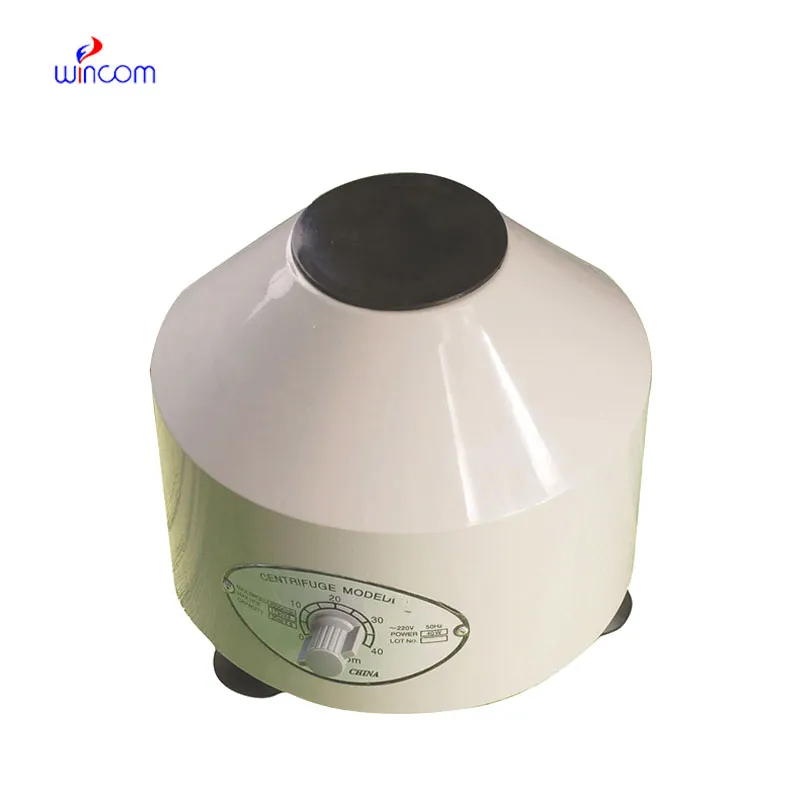
{Keywords} of the future will unprecedentedly advance in performance and design. Future systems will feature adaptive balancing technology that adjusts to dynamic loads in real time. Intelligent rotors will track stress and fatigue in real time, allowing for extended service life. With IoT connectivity, multiple large capacity refrigerated centrifuge factory units will be remotely managed to streamline laboratory networks. In biomedical applications, miniaturized devices will facilitate high-throughput screening with low sample volumes. These advancements are a step toward smarter, faster, and greener devices that revolutionize how separation processes are controlled in modern science.
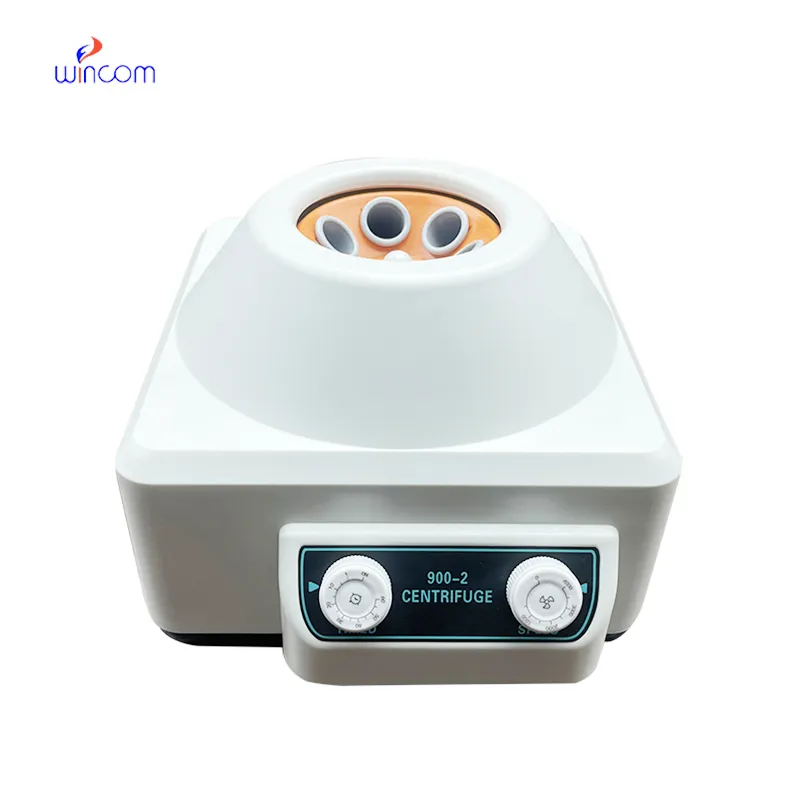
Proper maintenance and care of large capacity refrigerated centrifuge factory are essential for ensuring accuracy, safety, and long life. Regular checking of rotors for cracks and corrosion eliminates mechanical failure and imbalance. Users must clean the chamber with mild detergent and must not use abrasive chemicals that will damage surfaces. Regular calibration checks must be conducted to ensure speed accuracy. Greasing moving parts according to the manufacturer's recommendation increases motor life. Upon each use, samples need to be withdrawn at once, and open lids to prevent condensation. Periodic maintenance and records provide consistent operation.
A large capacity refrigerated centrifuge factory is a universal gadget designed to separate parts in a mixture through sheer spinning power. A large capacity refrigerated centrifuge factory operates through the principle of sedimentation, in which heavier particles move outwards and lighter particles remain at the center. Employed within laboratories, clinics, and industry in general, a large capacity refrigerated centrifuge factory may be utilized to separate materials such as blood plasma, proteins, and chemical reagents with accuracy. Modern large capacity refrigerated centrifuge factory exist in various forms, from benchtop to industrial types and ultracentrifuges, all for specialized applications. They are accurate and reproducible, a necessity in production and research.
Q: What safety measures are important when operating a centrifuge? A: Always ensure the rotor is balanced, the lid is securely closed, and safety locks are engaged before starting operation. Q: What types of centrifuges are available? A: Common types include micro, benchtop, refrigerated, and ultracentrifuges, each suited for specific laboratory or industrial applications. Q: Why is balancing samples important for a centrifuge? A: Imbalanced samples can cause vibration, noise, and mechanical stress, potentially damaging both the rotor and the instrument. Q: What materials can be processed in a centrifuge? A: A centrifuge can handle liquids, suspensions, and even some emulsions, depending on its speed and rotor type. Q: How long can a centrifuge run continuously? A: Run time depends on the model and workload—most can operate from a few minutes up to several hours under proper temperature control.
We’ve been using this mri machine for several months, and the image clarity is excellent. It’s reliable and easy for our team to operate.
The water bath performs consistently and maintains a stable temperature even during long experiments. It’s reliable and easy to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re interested in your delivery bed for our maternity department. Please send detailed specifica...
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko