In modern-day lab environments, the refrigerated high speed centrifuge manufacturer is not just a separation apparatus—it is precision engineering. With simple-to-view digital displays and microprocessor controls, it makes it easy for scientists to quickly adjust variables like acceleration and deceleration rates. Other models come equipped with onboard diagnostics that analyze rotor condition and operating performance. High-end safety features like automatic lid interlocks and imbalance detection offer protection at every cycle. With more rapid and consistent processing needed in industries, refrigerated high speed centrifuge manufacturer technology keeps up with stability, precision, and greater throughput capability.

From research in the laboratory to large-scale production, refrigerated high speed centrifuge manufacturer devices have a place in processes requiring precision and efficiency. They purify reaction mixtures and solvents in chemical production. Hospitals rely on refrigerated high speed centrifuge manufacturer for the testing of patients and therapeutic treatment. In farming, refrigerated high speed centrifuge manufacturer are used to study plant biology and develop fertilizer formulations. In brewing and winery operations, they provide consistency within products by filtering out impurities. Even environmental engineers rely on refrigerated high speed centrifuge manufacturer to filter sediment as well as identify contaminants. Such wide-ranging functionality demonstrates its vital position in contemporary technology and applied sciences.
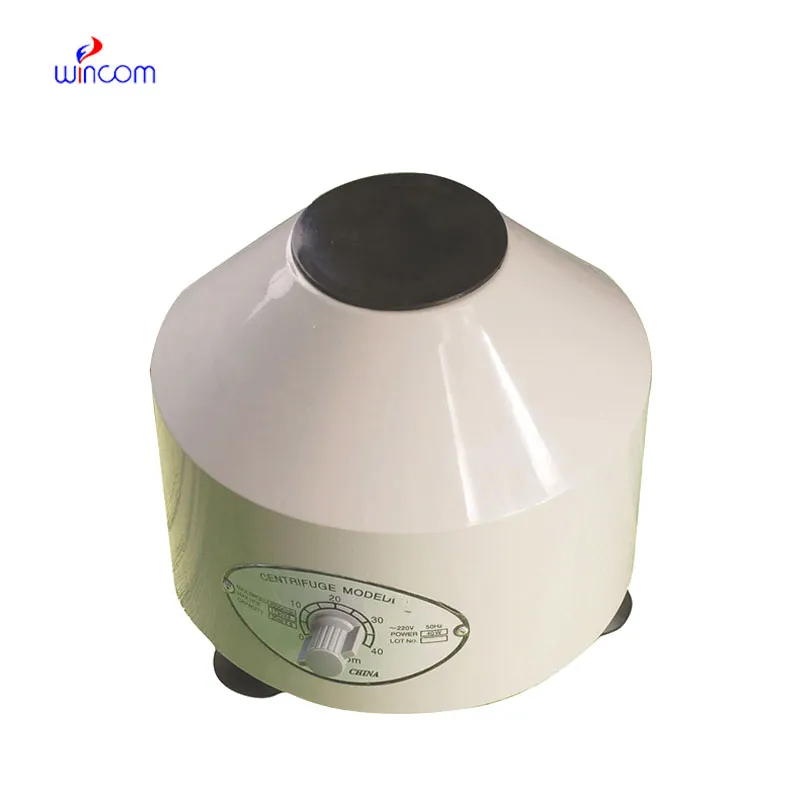
The refrigerated high speed centrifuge manufacturer of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, refrigerated high speed centrifuge manufacturer systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place refrigerated high speed centrifuge manufacturer at the forefront of international scientific advancement.
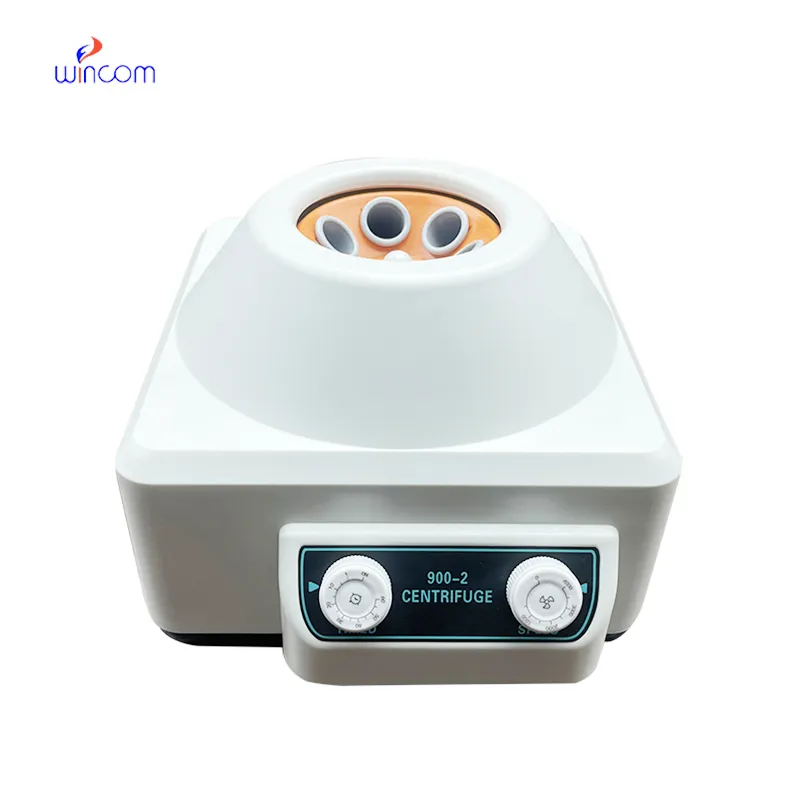
Proper care routines prolong the life of refrigerated high speed centrifuge manufacturer significantly. Operators should inspect the rotor for corrosion or scratches after each use and clean with non-abrasive substances. The lid and chamber should be free from residue to prevent contaminations. Frequent lubrication of mechanical interfaces ensures effortless movement. Temperature and humidity control in the storage room protect internal parts against damage. A maintenance record helps track service time and early wear detection. Ongoing maintenance of these factors allows refrigerated high speed centrifuge manufacturer to perform reliably for decades.
refrigerated high speed centrifuge manufacturer revolutionized laboratory and industry processes of substance separation forever. By speeding up the sample at high speed, they produce an immense force that separates mixtures based on particle density. This is the mechanism that enables efficient extraction of biological compounds, chemicals, and nanoparticles. Laboratories apply refrigerated high speed centrifuge manufacturer for analysis, purification, and research. In industry, they enable the refining of oil and food quality analysis. Small tabletop units and industrial units both use the same fundamental principle—precision with rotational energy and controlled acceleration.
Q: What are the main components of a centrifuge? A: Key components include the rotor, motor, control panel, safety lid, and chamber, each working together to achieve precise separation. Q: How can I verify that a centrifuge is functioning correctly? A: Check that the machine runs smoothly without any unusual vibrations or noises, check the speed accuracy and evaluate the results to ensure consistent separation. Q: Is it safe to open a centrifuge immediately after use? A: No, the device should come to a complete stop before opening to avoid injury or sample disruption. Q: How should a centrifuge be stored when not in use? A:Store it unplugged, covered, and in a dry, dust-free environment to protect internal components from moisture and corrosion. Q: Can centrifuge operation be automated? A: Yes, modern models include programmable controls and digital interfaces that allow automated speed, time, and temperature settings.
We’ve used this centrifuge for several months now, and it has performed consistently well. The speed control and balance are excellent.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We are planning to upgrade our imaging department and would like more information on your mri machin...
I’d like to inquire about your x-ray machine models. Could you provide the technical datasheet, wa...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko